Commercial Reverse Osmosis And Mineral Water Purification Plant About
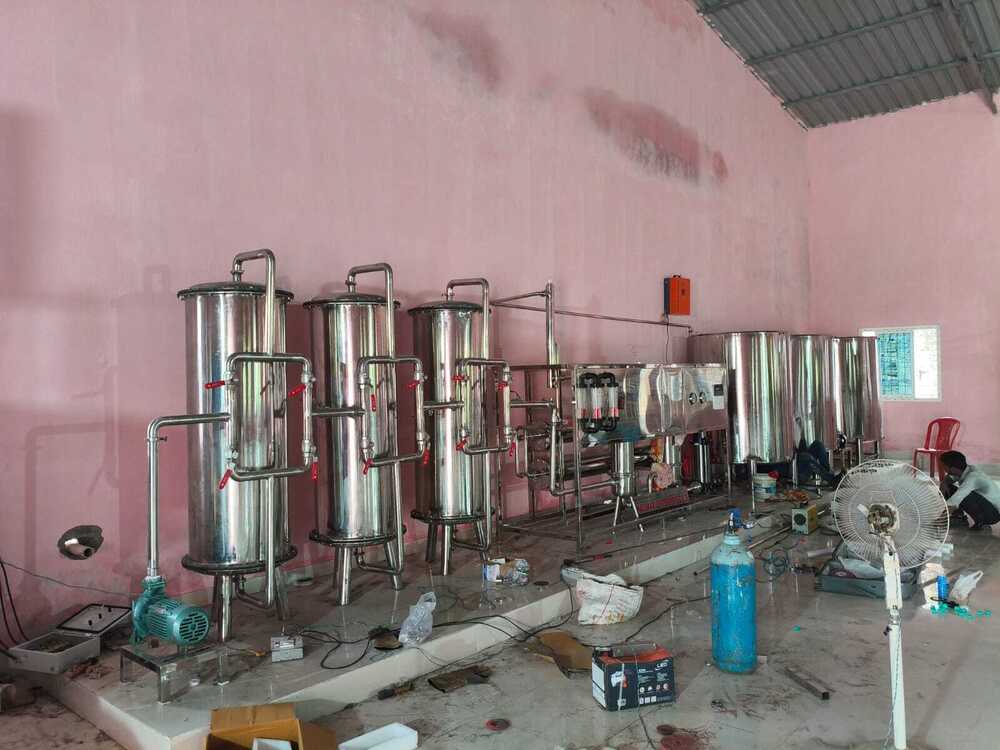
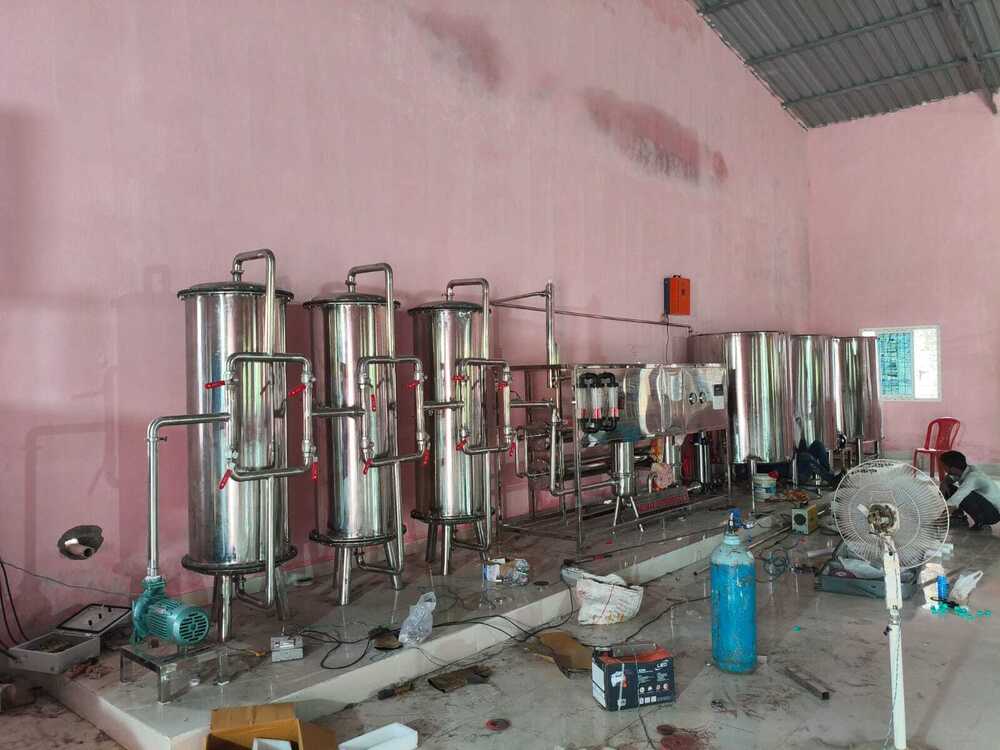
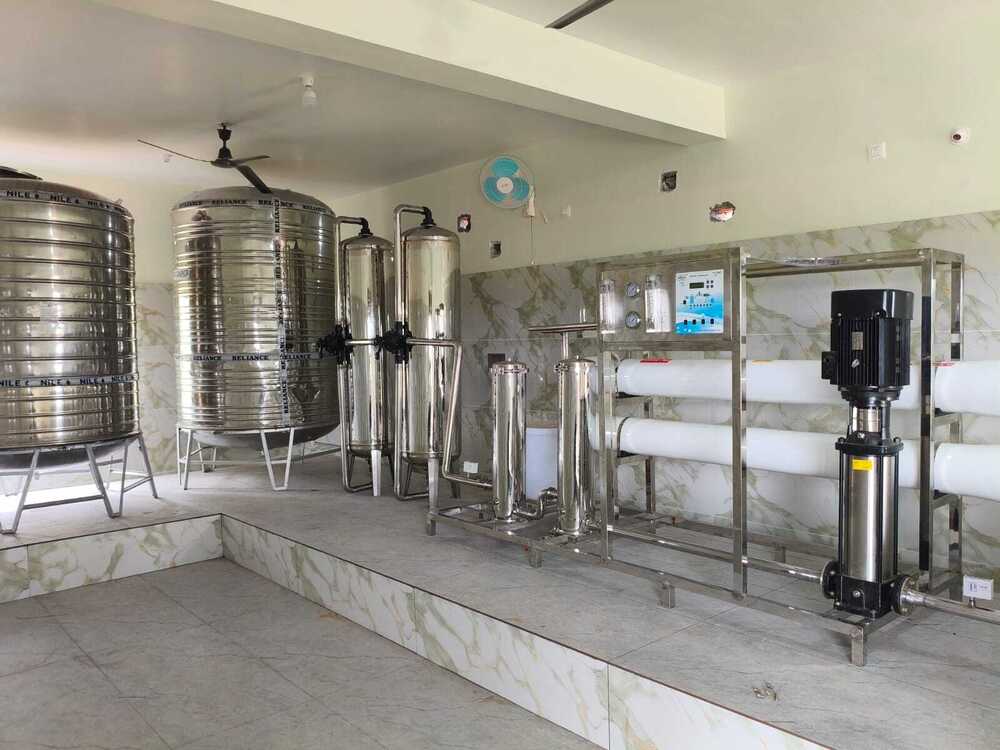
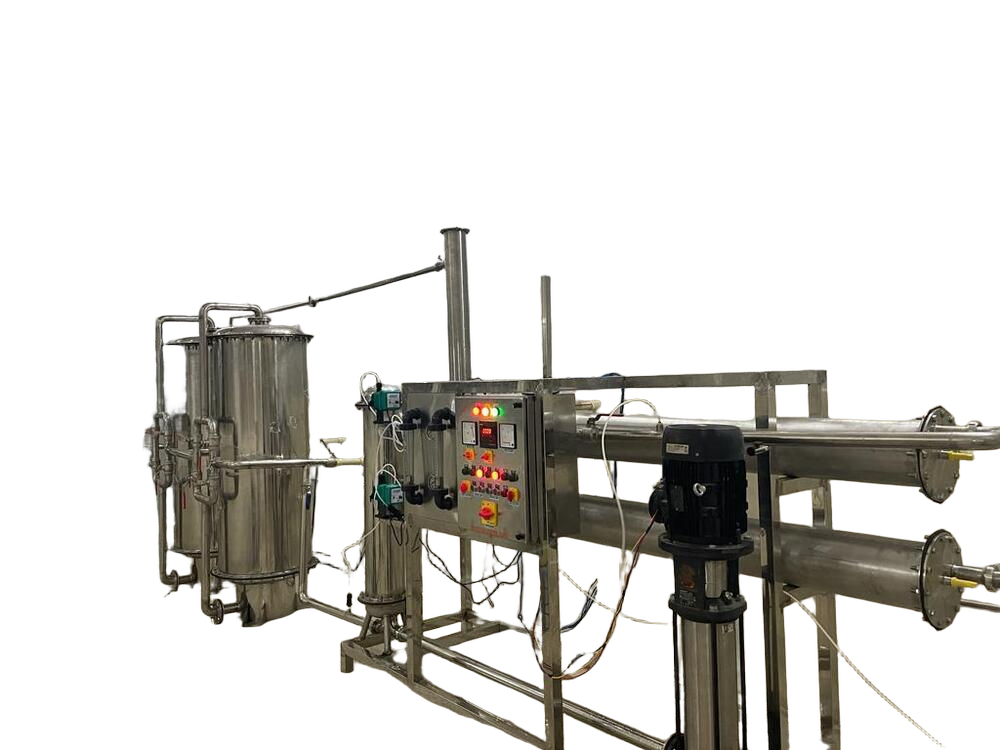
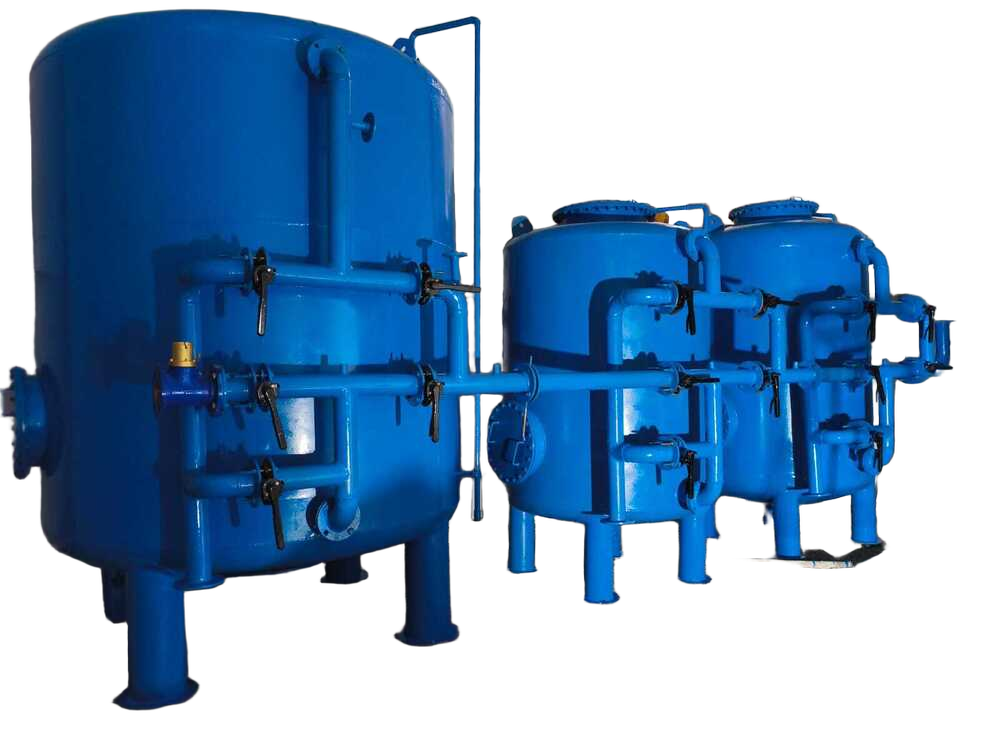
Redeem exceptional value with our Commercial Reverse Osmosis and Mineral Water Purification Plant, engineered for top-drawer performance and praiseworthy reliability. Benefit from instant savings and an unbeatable price-without compromising quality. With reputable DOW or Hydranautics membranes, digital/PLC control panels, and automatic CIP cleaning, this uncommon solution ensures up to 99% purity, 95-98% efficiency, and versatile output capacities (500-10,000 LPH). Built on stainless steel frames, it's compatible with UV/Ozone disinfection, supports various water sources, and guarantees water meeting BIS/WHO potability standards. Ideal for commercial, hospitality, and industrial needs across India.
Versatile, High-Efficiency Solution for Diverse Applications
The Commercial Reverse Osmosis and Mineral Water Purification Plant is ideally suited for commercial drinking water supplies, packaged water facilities, hotels, hospitals, and industrial applications. Its special features include advanced automatic cleaning, corrosion-resistant construction, adjustable pH, continuous or batch operation, and outputs that comply with BIS/WHO standards. Designed to handle borewell, river, municipal, or brackish water, this plant ensures consistently superior water quality, making it a vital solution for multiple sectors seeking dependable water purification.
Sample, Export, and Reliable Processing-Delivering on Every Promise
Sample units of the Commercial Reverse Osmosis and Mineral Water Purification Plant are available for quality verification. We serve multiple export markets, offering fully certified systems and streamlined order processing for swift delivery. Competitive sale prices, secure goods transport, and options for on-site installation-including training-make procurement seamless across India and export destinations. Our certifications testify to quality and performance, ensuring compliance with international water safety and efficiency standards.
FAQ's of Commercial Reverse Osmosis And Mineral Water Purification Plant:
Q: How does the Commercial Reverse Osmosis and Mineral Water Purification Plant ensure water of drinking quality?
A: This plant uses advanced RO membranes, digital/PLC controls, automatic cleaning, and UV or Ozone disinfection to consistently produce water meeting BIS/WHO potable standards, ensuring purity up to 99%.
Q: What special features set this water purification system apart from others in the market?
A: Built with stainless steel frames, it offers automatic CIP cleaning, corrosion resistance, high recovery and recycle rates, and supports a range of water sources with adaptability in capacity and operation mode.
Q: Where can this purification plant be installed and used efficiently?
A: Suitable for packaged drinking water plants, hotels, hospitals, industries, and commercial facilities, it is designed for floor or skid mounting and works efficiently with borewell, municipal, river, or brackish water sources.
Q: What is the process for ordering and receiving the plant?
A: Order processing is streamlined for fast turnaround. After order confirmation, goods transport and on-site installation (with training) are provided, ensuring a smooth and secure setup.
Q: What are the main benefits of using this commercial RO plant?
A: Key benefits include high efficiency (95-98%), adjustable output to meet operational needs, reliability, robust build for long service life, and compliance with leading safety standards for potable water.




 Send Inquiry


 Send Inquiry
